How to choose a supply chain strategy for unpredictable demand
Choose a supply chain strategy by comparing how quickly demand changes with how quickly supply can respond. Lean operations suit products with a dependable demand base and reliable replenishment. Agile operations justify their additional cost when shortages are expensive and supply can adjust within the required delivery window. A hybrid approach fits situations where common materials remain predictable while finished-product demand varies.
The choice should be made at product-family or component level. Applying one model across an entire portfolio often produces excess stock in slow-moving variants while leaving critical items exposed. Begin with the customer’s acceptable waiting time, the actual replenishment cycle, and the financial consequences of being wrong.
Start with the gap between demand and response time
The most useful starting point is the gap between the time customers will wait and the time required to replenish supply. Include order processing, material availability, production queues, inspection, transport, customs clearance, and final delivery. A quoted factory lead time covers only part of this cycle.
If customers require delivery before replenishment can finish, some commitment must occur before the order arrives. That commitment might be finished inventory, common components, reserved capacity, or a combination. If customer waiting time exceeds the reliable fulfillment cycle, production against confirmed orders becomes more practical.
Measure lead-time variation alongside its average. A route with an attractive average transit time but frequent extended delays requires a different inventory policy from a consistently slower route. For cross-border sourcing, compare the distribution of actual receipt dates with promised dates, including inspection holds and documentation corrections.
Demand data also needs interpretation. Recorded sales understate demand during stockouts, while large orders placed before announced price increases can exaggerate recurring consumption. Separate normal demand from promotions, project orders, cancellations, and purchases brought forward. Otherwise, a strategy intended to absorb uncertainty may be built around misleading signals.
Two patterns deserve different treatment: fluctuating order quantities for a regularly purchased item, and intermittent demand with long gaps between orders. The second pattern creates a greater risk of holding inventory that remains unused. Averages and percentage-based forecast errors alone are poor guides when many periods contain zero demand.
Where lean, agile, and hybrid strategies fit
Lean remains useful within unpredictable markets when a dependable base load exists. Stable consumption can run through an efficient supply channel while uncertain demand receives separate treatment. Lean becomes fragile when low inventory is pursued without dependable replenishment or a credible response to demand exceeding the plan.
Agility requires an executable response. Shorter planning meetings and frequent forecast updates achieve little if raw materials take longer to obtain than customers will wait. Flexible supply has value only when material, production, qualification, and logistics constraints all permit the required adjustment.
A hybrid supply chain strategy often fits portfolios with stable aggregate demand but unstable variant demand. Total demand for a product family may be reasonably predictable even when individual sizes, finishes, or configurations are not. Shared inventory can absorb that mix uncertainty, provided conversion remains fast enough.
Place the inventory buffer before demand becomes specific
The position where supply changes from forecast-driven activity to order-driven activity determines what inventory must protect. Holding finished goods offers fast dispatch but exposes each variant to forecasting error. Holding common materials pools some uncertainty, although the remaining processing time still has to fit the delivery promise.
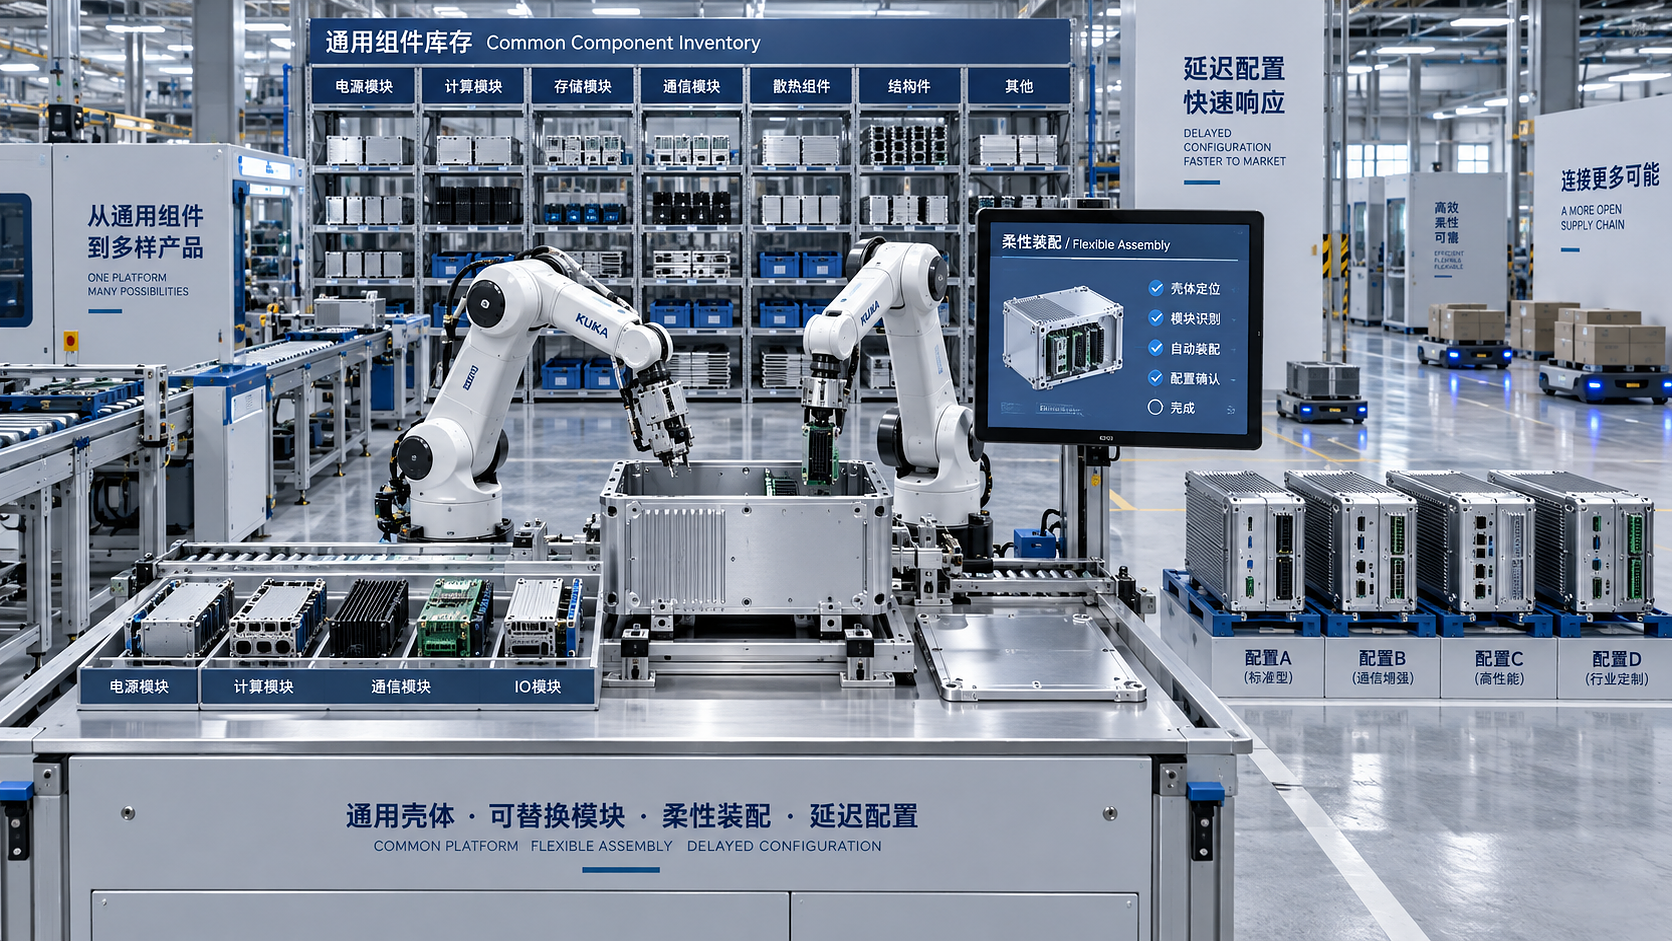
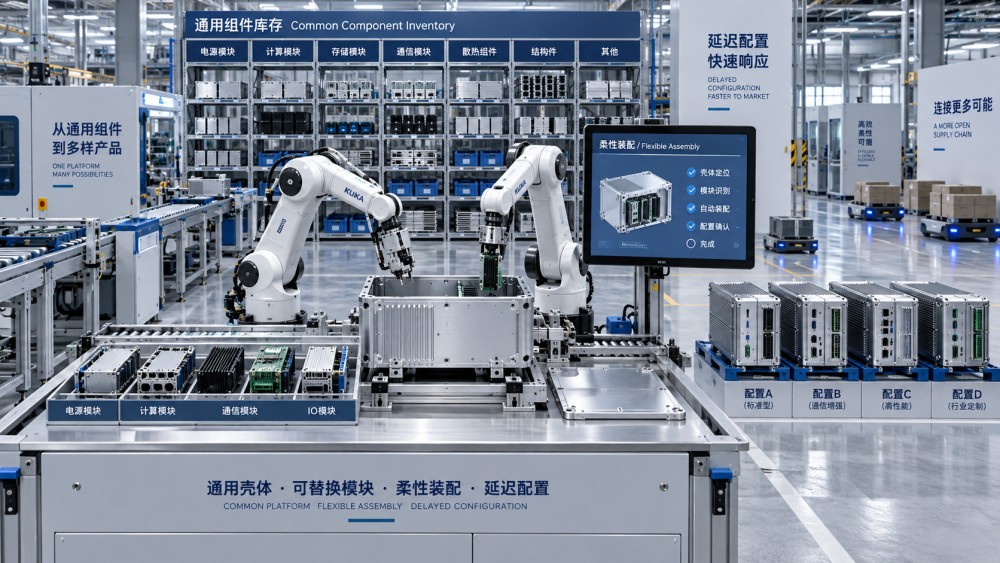
Consider a configurable industrial assembly using a common housing and several optional modules. Stocking the housing and delaying module installation reduces commitment to individual configurations. This approach works only if assembly, testing, labeling, and release can be completed within the available delivery window.
Postponement is less useful when differentiation occurs early. An alloy grade, custom casting geometry, or dedicated surface treatment may be fixed before a long production cycle begins. Generic stock then provides little protection against demand for the wrong specification. The useful buffer must be a technically valid input for the products it is intended to support.
Physical suitability sets further limits. Shelf life, corrosion protection, moisture sensitivity, traceability, and storage conditions determine whether materials can remain available until demand becomes clear. Pooling inventory across variants also requires compatible specifications; similar appearance does not establish interchangeability.
For products with expensive finished stock and short final processing, postponement deserves serious evaluation. Where final completion requires lengthy curing, specialist testing, or scarce equipment, capacity reservations or selected finished-goods buffers may provide better protection.
Verify flexibility before paying for it
Supplier flexibility should be expressed as operating terms. Relevant evidence includes the permitted volume range, notice period for changes, minimum batch, order-freeze date, and time required to recover from a demand surge. A general promise to “support urgent orders” leaves the most important constraints unresolved.
Capacity availability must include upstream materials and shared production assets. A supplier with spare assembly capacity can still be unable to deliver if a critical component is allocated elsewhere. Similarly, a second supplier offers limited resilience when both sources depend on the same sub-tier factory, transport corridor, or specialized tooling.
Alternative supply also has a readiness cost. Tooling transfer, sample approval, process validation, and customer acceptance can delay activation. An approved source with recent production experience provides a different response capability from a supplier listed in a database but never used.
Commercial terms decide who carries uncertainty. A blanket order with flexible releases might improve replenishment while still requiring payment for unused material. Consignment changes ownership arrangements, but contractual liability for obsolete stock can remain. Compare cancellation rights and material commitments alongside quoted prices.
- Reserved capacity: Establish what output is protected, which materials are included, and whether that capacity remains available during wider market shortages.
- Volume adjustments need a defined notice window. Flexibility offered after the customer’s delivery deadline has little service value.
- Transport alternatives: Confirm shipment eligibility, packaging requirements, and usable route capacity before treating expedited freight as a recovery option.
Evaluate the economics under both excess and shortage
Compare strategies using total relevant cost over the same planning horizon. Include landed purchase cost, inventory financing, storage, handling, expected obsolescence, capacity reservations, and emergency replenishment. Keep assumptions consistent so that one option is not assessed with average demand while another carries the full stress scenario.
The cost of a shortage depends on its consequence. A delayed sale, a canceled order, and a production interruption have different economics. Lost revenue is also different from lost contribution margin. Where demand shifts to a later period, counting the entire order value as a permanent loss overstates the case for extra inventory.
Inventory has unequal protective value. An inexpensive component that blocks completion of a high-value assembly may justify more coverage than its purchase price suggests. Expensive, specialized finished goods with low substitution potential require closer attention to obsolescence and recovery value.
Service measures should match the delivery promise. Unit fill rate shows how much demand ships immediately; complete-order delivery exposes shortages that prevent an entire order from shipping. A strong aggregate result can hide repeated failures in a critical product family, so evaluate service at the level where shortages cause consequences.
Use demand upside, demand downside, and supply-delay scenarios to compare the choices. For each, calculate the inventory remaining, unfilled demand, recovery time, and cash committed. Include a combined demand surge and supply delay when that combination is plausible. Scenarios are stress tests rather than predictions.
An agile option earns its premium when its response capability reduces costly shortages or excess commitments enough to justify the added expense. A lean option remains attractive where the demand base is stable and deviations are manageable. Hybrid economics depend heavily on how much stock can remain common and how quickly it can become saleable output.
Turn the chosen model into operating rules
A strategy becomes usable when it specifies the action taken after demand changes. Define which orders enter the stable production schedule, which draw from inventory, and which trigger flexible capacity. Set the point beyond which confirmed production cannot change without explicit approval of the cost and delivery consequences.
For a hybrid model, distinguish base demand from the uncertain increment. The base can follow scheduled replenishment, while the increment uses common stock, reserved capacity, or a faster supply route. Avoid defining the base from an unusually strong recent period; temporary peaks can otherwise become permanent purchasing commitments.
Inventory settings should reflect uncertainty during the replenishment and review period. Increasing a forecast alone does not correct unreliable lead times. Similarly, applying the same weeks-of-cover target to every item ignores differences in demand frequency, substitution, shelf life, and shortage impact.
Set escalation triggers against observable conditions: expected stockout before the next usable receipt, demand exceeding verified response capacity, or excess inventory accumulating beyond the agreed holding horizon. Assign authority for expediting, reallocating stock, changing delivery promises, and accepting cancellation costs. Waiting for successive approvals can consume the response time the strategy was designed to preserve.
Test the decision where its assumptions are weakest
Pilot the proposed approach on a bounded product family with visible demand, inventory, and receipt data. Include a meaningful constraint, such as variable supplier lead time or several finished variants sharing a component. A pilot containing only easy-to-replenish items will reveal little about resilience.
Track complete-order service, inventory aging, emergency freight, schedule changes, and actual replenishment time. Interpret them together. Better service funded by persistent expediting indicates a different result from better service achieved through the intended inventory and capacity policy.
The review should identify which assumption failed. If common stock accumulates while finished orders remain late, final conversion capacity may be the bottleneck. If reserved capacity sits idle because materials are unavailable, the agreement protects the wrong stage. If slow-moving variants absorb cash despite stable family demand, differentiation may still occur too early.
Expand the model only after its response mechanism has worked under the conditions it is meant to address. Revisit the choice when lead times, product design, customer delivery expectations, or supplier commitments change; each can move the most effective inventory and capacity buffer to a different point in the chain.
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.
Recommended News
 Supply ChainOct 15, 2026How to choose a supply chain strategy for unpredictable demand
 Supply ChainOct 14, 2026How to assess an industrial equipment supplier's spare parts support
 Supply ChainOct 14, 2026EU Updates CSDDD Guidance on Global Supply Chain Due Diligence
 Global SourcingOct 13, 2026How to assess industrial automation suppliers for legacy integration